




 Knowledge Hub
3D printing car in additive manufacturing: how the automotive industry is rethinking production

août 2026
3D printing car in additive manufacturing: how the automotive industry is rethinking production
août 2026

Tooling costs, long lead times, and rigid supply chains have shaped how cars get built for decades. Robotic LFAM and WAAM are quietly rewriting those rules. From full bodywork printed straight from CAD to metal suspension components and molds produced without a single machining pass, large scale 3D printing has moved well past the prototype stage. This article looks at where 3d printing car manufacturing actually delivers, with real projects and hard numbers behind the claims.
Why the additive manufacturing car conversation finally matters to engineers
For years the pitch around the additive manufacturing car sounded good on paper and fell apart on the shop floor: build volumes too small, feedstocks too weak, deposition rates nowhere near what a production line demands. That gap has narrowed, and in some niches it’s gone entirely.
The shift comes down to a few things landing at once. Large format additive manufacturing (LFAM) platforms now handle envelopes measured in meters, with pellet-fed extrusion running nozzle diameters in the 5–8 mm range and deposition rates that make multi-meter parts viable in tens of hours. Fiber-reinforced thermoplastics — ABS with carbon fiber, PETG with glass fiber — deliver the specific stiffness automotive work actually requires. And robotic kinematics matter more than most people expect: a multi-axis arm can orient the deposition plane freely, so toolpaths follow the part geometry instead of fighting it, which is where fixed-axis gantries hit their limit.
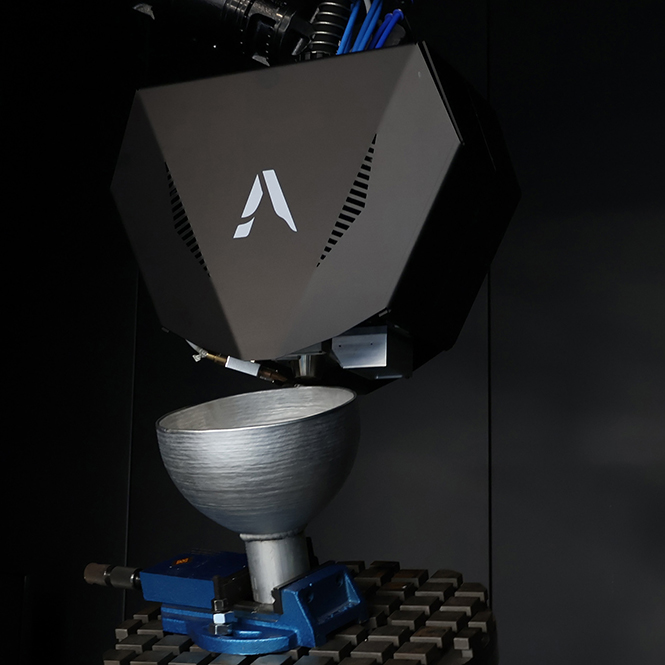
What draws technical decision makers is the removal of tooling. Conventional fabrication of a custom body panel or a complex bracket means molds, fixtures, machining time, and weeks of waiting before the first usable part exists. Skip that, and you compress the entire timeline. Caracol, a European company working in the advanced manufacturing industry, frames its whole approach around three levers most plant managers care about: flexibility, efficiency, and sustainability. Its Heron AM platform covers composite robotic LFAM, Vipra AM handles large scale metal parts via WAAM, and Eidos Manufacturing ties the workflow together from slicing to production.
What 3d printing in car industry looks like in real projects
Consider a scale hypercar prototype that Cross Industry Dynamics needed ready for a Las Vegas trade show. The brief was brutal: sketch to finished, exhibition-grade vehicle in two weeks. Using robotic LFAM, the team went straight from the digital model to deposition, skipping the tooling and mold-making that conventional fabrication would have demanded. The full body and every ancillary component came off the cell in 24 hours of continuous print time, on a body measuring roughly 1.6 × 2.9 × 1.4 m and weighing 85 kg.
What that bought them:
- 100% of tooling and mold cost eliminated on a body that would only ever be built once.
- Print phase down to ~7% of the total project window — 24 hours out of 14 days.
- ~93% of the schedule left for finishing, the assembly and sanding work that can’t be compressed without the quality showing.

Castelletto Circuit took a different angle. Instead of a one-off show piece, they produced the entire bodywork for a custom Legend Car racing category through large scale 3D printing: ABS reinforced with 20% carbon fiber, sliced directly from CAD, 173 kg of parts across roughly 150 hours of deposition, assembling into a body 3.6 m long. Structural duty sat with the internal rollbar frame, which kept the bodywork itself an unstressed set of near-net-shape panels.
The measurable side of it:
- Lead time cut by up to 50% against traditional manufacturing.
- 100% of bodywork printed direct from CAD — zero tools, zero molds, zero CNC machining.
- Curing ovens and multi-stage tooling removed entirely (100%), which drops energy draw across the process chain.

Then there’s the tooling-for-tooling case, which is where a lot of skeptical manufacturers get won over. Duqueine Automotive applied robotic LFAM to produce direct molds for racing car parts, printing the tool instead of milling it. That takes an entire machining cycle off the critical path, and it changes the economics of iteration: a revised mold becomes a reprint rather than a re-machine. Downstream nothing else moves — the layup process the team already runs stays exactly as it is.
Speed isn’t the only payoff. THE CAB, developed with LG Project Management, is the first functional RV living module printed as a single monocoque in recycled polymer — rPETG reinforced with glass fiber and UV-stabilized, 660 kg, 4.3 × 2.1 × 2.1 m, laid down in 92 hours on a rail-mounted robotic LFAM cell running an 8 mm nozzle.
The numbers that make it interesting to a production manager:
- Lead time down roughly 92% — one week with LFAM against approximately three months via conventional production.
- Material waste cut by around 60% compared with fiberglass lamination.
- 100% of molds, adhesives and multi-component assembly removed, since the shell prints as one uninterrupted piece.
- 92 hours of print time ≈ 55% of the total one-week window, leaving the rest for sanding and painting.
- Cavities and service channels integrated directly into the print, so electrical, plumbing and heating installation loses both routing time and potential failure points.

If you want the process side in more depth — qualification logic, post-processing chains, where the technology stops being a prototyping tool and starts producing parts that ship — Caracol has put it together in a dedicated resource on robotic LFAM for end-use parts in the transportation industry: Read the White Paper!
Additive manufacturing car parts: from bodywork to functional metal
Bodywork and prototypes are the visible wins. The quieter, arguably more significant story is functional additive manufacturing car parts — the ones that carry load and have to survive real duty cycles.
Metal is where this gets serious. NP Aerospace, working with the Digital Manufacturing Centre, produced a Mastiff suspension and differential carrier on Vipra AM, substituting WAAM for the usual casting and forging route. A structural 110 kg part in ER100, 540 × 500 × 500 mm, deposited in about 60 hours, then heat treated and finish machined.
What the switch delivered:
- Lead time reduced by up to 50% versus the conventional manufacturing route.
- 100% of tooling cost eliminated, which is what makes low-volume runs and development iterations economically defensible.
- Full performance envelope met with no change to the functional specification.
- 60 hours of deposition for a 110 kg load-bearing component, extreme overhangs included, thanks to coordinated multi-axis positioning of both robot and workpiece.
Additive still won’t replace stamping lines churning out a hundred thousand identical panels, and nobody serious is claiming otherwise. Where robotic LFAM and WAAM earn their place is the long tail: customization, low volumes, rapid iteration, and the growing pull toward supply chains that don’t collapse when one supplier goes quiet.
For anyone weighing whether to bring 3d printing car manufacturing in-house or through a service partner, the honest advice is to start narrow. Pick the part that’s killing your lead time or your tooling budget, run it through large scale 3D printing, measure the delta. The case studies above didn’t begin as factory-wide transformations. They started with one stubborn problem and a machine that happened to solve it better.
Want to see whether your next large-scale automotive part can be printed?
LFAM FOR THE AUTOMOTIVE INDUSTRY
Discover how to use Caracol’s large-scale 3D printing technology for your automotive applications. Register here to download the whitepaper.
Articles Knowledge Hub connexes
En savoir plus sur les technologies LFAM
-

Knowledge Hub. Robotic LFAM for end-use parts in the transportation industry
-

Knowledge Hub. What Is Rapid Prototyping in 3D Printing? Methods, Examples, and Where Prototyping Ends
-

Knowledge Hub. Why the advantages of robotics in manufacturing start in the classroom
-

Knowledge Hub. Robotic automation in manufacturing: how industrial robots are reshaping modern production
-

Knowledge Hub. 3D printing in defense: how robotic LFAM and WAAM are redefining industrial dual-use production
-

Knowledge Hub. How to build a robotic LFAM Microfactory – the final tutorial
-

Knowledge Hub. The microfactory model: robotic additive manufacturing for flexible industrial production
-

Knowledge Hub. Metal 3d printing: challenges & scalability
-

Knowledge Hub. Industry 5.0 vs Industry 4.0: key differences and what changes for manufacturing
-

Knowledge Hub. On-demand manufacturing: what it is, how it works, and some examples
-

Knowledge Hub. How is 3d printing used in architecture?
-

Knowledge Hub. Carbon Fiber Composite Manufacturing at Scale: How Robotic LFAM Redefines Composites
-

Knowledge Hub. What 3D Printer Design Software to Use for Large Format Robotic Systems: A Complete Guide
-

Knowledge Hub. 3D Printing in Automotive Manufacturing, Aviation, and Mass Production: How AM Is Reshaping Mobility
-

Knowledge Hub. Best practices for Design & Production with robotic LFAM
-

Knowledge Hub. Integrating robotic process automation (RPA) for strategic growth in modern advanced manufacturing
-

Knowledge Hub. Robotic large format additive production for Jigs & Molds
-

Knowledge Hub. Robotic large format additive production for Marine Applications
-

Knowledge Hub. Robotic large format additive production for the Automotive Industry
-

Knowledge Hub. Robotic additive production for Design & Architecture
-

Knowledge Hub. Applications of 3D Printing in Aerospace and Defense
-

Knowledge Hub. Distributed Manufacturing: Building Resilient, Flexible Supply Chains
-

Knowledge Hub. Metal Additive Manufacturing Market: Technologies & Processes for Demanding Industries
-

Knowledge Hub. Robotics and Automation transform industries: a look into the Future of Manufacturing
-

Knowledge Hub. 3D printing Architectural Elements for Building
-

Knowledge Hub. Empowering industrial production with live data: the growing role of IoT in LFAM
-

Knowledge Hub. How is 3d printing used in the automotive industry?
-

Knowledge Hub. What is Advanced Manufacturing? How technology improves industrial manufacturing
-

Knowledge Hub. Why adopt thermoplastic 3d printing materials for advanced industrial applications
-

Knowledge Hub. Strengths and weaknesses of the 3 most common 3D printing materials
-

Knowledge Hub. Industry 4.0 & additive manufacturing: delivering efficiency and sustainability in production
-

Knowledge Hub. The rise of 3D printed furniture: leveraging LFAM to revolutionize the design industry
-

Knowledge Hub. The future of LFAM: integration at its core
-

Knowledge Hub. The benefits of 3D printing aircraft parts
-

Knowledge Hub. How does 3D printing help the environment?
-

Knowledge Hub. Innovation in the marine industry: 3D printing boat structures and components
-

Knowledge Hub. Pellet 3D printing and its benefits compared to 3D filament extruders
-

Knowledge Hub. Guidelines for large format 3d printing
-

Knowledge Hub. Sustainability in the automotive industry through LFAM
-

Knowledge Hub. What is robotic LFAM 3D printing?
-

Knowledge Hub. Beyond rapid prototyping 3D printing, towards industrial production with LFAM
-

Knowledge Hub. Engineering the future of manufacturing through LFAM